
Introduction
In the global food processing and cold chain industry, processing rooms (+10℃ to +18℃) play a crucial role in ensuring hygiene, safety, and temperature stability during food preparation and handling.
Unlike cold storage or freezer environments, a processing room is designed for controlled ambient conditions, allowing safe handling of meat, seafood, dairy, bakery products, and ready-to-eat food in compliance with international hygiene standards.
As food safety regulations become stricter worldwide, the demand for high-quality industrial food processing rooms is rapidly increasing.
This article provides a complete guide to the top 15 processing room manufacturers in the world, covering system structure, applications, technical design, and key selection criteria for industrial buyers.
What Is a Processing Room (+10℃ to +18℃)?
A processing room is a temperature-controlled food preparation environment designed to operate between +10℃ and +18℃, ensuring optimal conditions for hygienic food handling.
It is widely used in industries where raw materials must be processed under controlled temperature conditions to prevent contamination and maintain product quality.
Typical applications include:
Meat cutting and deboning
Seafood processing
Dairy product handling
Bakery and pastry production
Central kitchen food preparation
Why Processing Rooms Are Important
Processing rooms are essential in modern food production systems because they:
Maintain food hygiene and reduce bacterial growth
Ensure stable working environment for operators
Improve product quality consistency
Comply with HACCP and international food safety standards
Reduce cross-contamination risks
How a Processing Room Works
A processing room maintains controlled temperature and airflow through:
Precision refrigeration systems
Air circulation and ventilation units
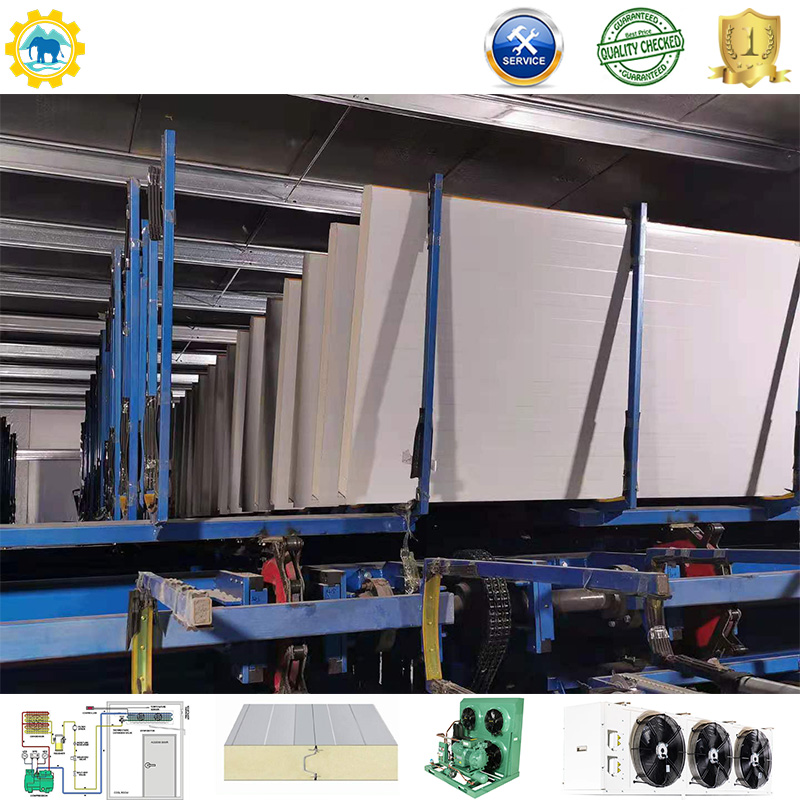
Hygienic insulated wall and ceiling panels
Temperature monitoring and control systems
Unlike cold storage rooms, processing rooms focus more on air hygiene, airflow design, and operational cleanliness rather than long-term storage.
Processing Room Structure and Components
Insulated Wall Panels
High-density PU/PIR panels provide:
Thermal stability
Anti-bacterial surface coating
Easy cleaning performance
Refrigeration and Cooling System
Includes:
Air-cooled or water-cooled condenser
Cooling coil units
Fan systems for uniform air distribution
Hygienic Flooring System
Designed with:
Anti-slip surfaces
Drainage systems
Water-resistant coating
Temperature Control System
Modern systems include:
Digital temperature controllers
Real-time monitoring
Alarm systems for abnormal conditions
Types of Processing Rooms
Meat Processing Room
Used for cutting, trimming, and packaging meat products under controlled hygiene conditions.
Seafood Processing Room
Designed for fish cleaning, filleting, and packaging.
Dairy Processing Room
Used for milk, cheese, butter, and yogurt production handling.
Bakery Processing Room
Supports dough preparation and pastry production.
Central Kitchen Processing Room
Used in hotels, restaurants, and catering facilities.
Processing Room vs Cold Room vs Freezer Room
Type | Temperature | Purpose |
|---|---|---|
+10℃ to +18℃ | Food preparation | |
Cold Room | 0℃ to +10℃ | Fresh storage |
Freezer Room | -15℃ to -30℃ | Frozen storage |
Top 15 Processing Room Manufacturers in the World
Below are globally recognized companies providing industrial refrigeration, HVAC systems, and food processing solutions.
1. Carrier Commercial Systems (USA)
A global leader in HVAC and refrigeration systems, providing temperature control solutions for food industries.
2. Johnson Controls (USA)
Offers integrated building and food processing environment control systems.
3. Daikin Industries (Japan)
Known for advanced air conditioning and precision temperature control technologies.
4. GEA Group (Germany)
Specializes in industrial food processing engineering and hygiene systems.
5. BITZER (Germany)
A leading compressor manufacturer widely used in processing room refrigeration systems.
6. Danfoss (Denmark)
Provides intelligent control systems for energy-efficient processing environments.
7. Mayekawa (Japan)
Focuses on industrial refrigeration and hygienic food processing technology.
8. LU-VE Group (Italy)
Specializes in heat exchange and air cooling systems for industrial applications.
9. Evapco (USA)
Manufacturer of cooling and heat rejection systems used in industrial facilities.
10. Frascold (Italy)
Known for compressor systems used in food processing refrigeration.
11. Hussmann (USA)
Provides commercial refrigeration and food retail processing solutions.
12. SCM Frigo (Italy)
Specializes in CO₂-based refrigeration and energy-efficient systems.
13. Heatcraft Worldwide Refrigeration (USA)
Offers commercial refrigeration systems for food industry applications.
14. Blue Star Limited (India)
Provides HVAC and industrial cooling solutions for food processing facilities.
15. Kaideli Processing Room Solutions (China)
Kaideli Refrigeration is a professional manufacturer specializing in industrial processing rooms (+10℃ to +18℃) and integrated food production environment systems.
Unlike standard HVAC suppliers, Kaideli focuses on complete engineering solutions, including design, manufacturing, and installation of hygienic food processing environments.
Company Overview
Kaideli delivers full turnkey solutions for food processing facilities, including:
Meat processing environments
Seafood handling rooms
Central kitchen preparation areas
Dairy processing systems
Bakery production rooms
Engineering Strengths
Kaideli processing rooms are designed with:
Precise temperature control (+10℃ to +18℃ stability)
Hygienic stainless steel and PU panel systems
Anti-bacterial wall and ceiling surfaces
Optimized airflow and ventilation systems
Easy-clean industrial flooring design
Global Project Experience
Kaideli has delivered processing room projects in:
Southeast Asia food factories
Middle East central kitchens
Africa meat processing plants
Europe food production facilities
Why Global Clients Choose Kaideli
Stable hygienic temperature control
Food safety compliant design (HACCP ready)
Fast modular installation
OEM & ODM customization capability
Factory direct supply advantage
Why Kaideli Competes in the Global Market
Kaideli is not just a component supplier—it provides complete food processing room engineering solutions.
Key advantages include:
Turnkey project capability
Custom engineering design
Competitive factory pricing
Fast delivery and installation
Strong export experience
Applications of Processing Rooms
Meat Industry
Ensures hygienic cutting, trimming, and processing.
Seafood Industry
Maintains freshness during handling and packaging.
Dairy Industry
Supports controlled production of dairy products.
Bakery Industry
Provides stable environment for dough preparation.
Central Kitchens
Used in hotels, restaurants, and catering industries.
Global Project Cases
Southeast Asia Meat Processing Facility
Large-scale hygienic processing room for export production.
Middle East Central Kitchen Project
High-capacity food preparation environment system.
Africa Seafood Processing Facility
Designed for coastal seafood handling operations.
Europe Food Production Plant
Hygienic processing system compliant with strict regulations.
Why Clients Trust Kaideli Processing Rooms
Stable +10℃ to +18℃ Control
Ensures consistent food-safe environment.
Hygienic Design
Easy-clean surfaces reduce contamination risks.
Energy Efficient Operation
Optimized cooling and airflow systems.
Fast Installation
Modular structure reduces construction time.
How to Choose a Processing Room Manufacturer
Key factors include:
Hygiene and food safety compliance
Temperature stability performance
Airflow and ventilation design
Material quality and durability
After-sales service and technical support
Processing Room Cost Factors
Room size and layout
Cooling system configuration
Material selection (PU panels, stainless steel)
Installation complexity
Custom engineering requirements
Energy Efficiency Technologies
Modern processing rooms use:
High-efficiency cooling systems
Smart temperature control systems
Optimized airflow distribution
Energy-saving insulation panels
Maintenance and Operation Tips
Regular cleaning and sanitization
Temperature monitoring
Air system maintenance
Equipment inspection
Frequently Asked Questions (FAQ)
What is the ideal temperature for a processing room?
Between +10℃ and +18℃ depending on application.
What industries use processing rooms?
Food processing, central kitchens, dairy, seafood, and meat industries.
What is the difference between processing room and cold room?
Processing rooms are for food preparation, cold rooms are for storage.
How much does a processing room cost?
Depends on size, design, and system configuration.
Can processing rooms be customized?
Yes, fully customized engineering solutions are available.
What is the lifespan of a processing room?
Typically 10–20 years depending on maintenance.
Conclusion
Processing rooms are a critical part of modern food production systems, ensuring hygiene, safety, and temperature stability during food handling.
As global demand for food safety increases, manufacturers like Kaideli Refrigeration provide reliable, customized, and energy-efficient processing room solutions for international markets.
Choosing the right manufacturer is essential for ensuring long-term operational efficiency and food safety compliance.
Connect with me: If you are planning a cold storage project or need expert guidance on selecting the right solution for your business, feel free to reach out. I am always happy to share insights from my years of experience in this industry.
Mr. Bruce Zhuang — Project Management Director
Cell / WhatsApp / WeChat: +86 189 6123 0696
✉️ manager@freezercold.com
Related News
-
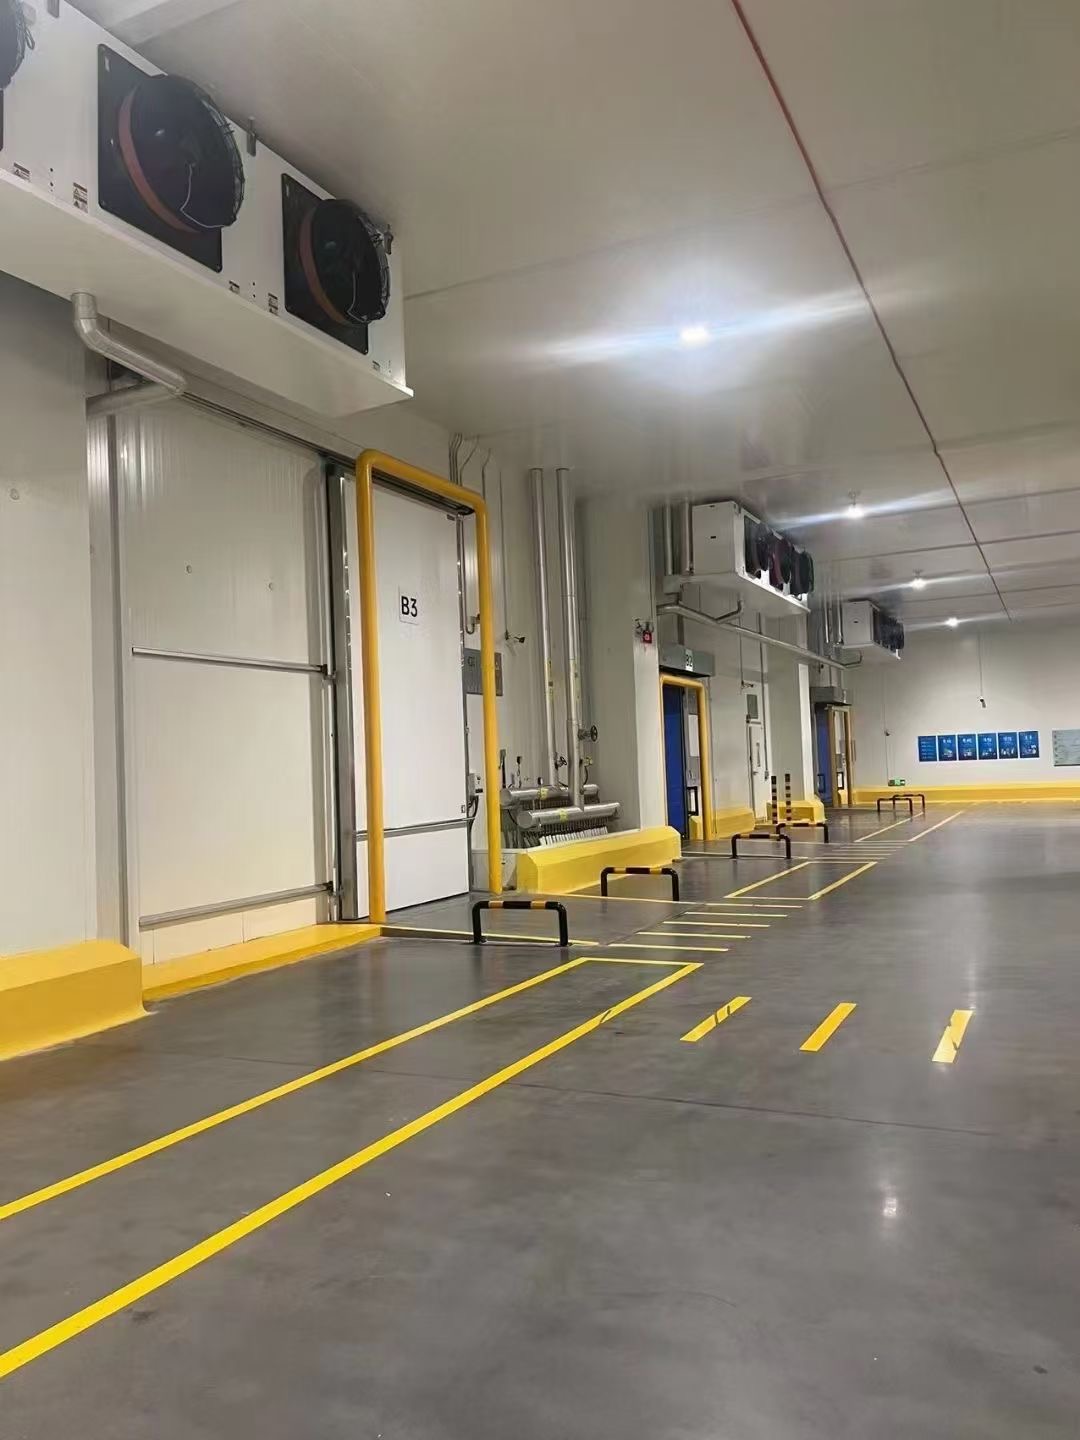 Project OverviewKAIDELI successfully completed a seafood cold storage project in Vietnam, providing a complete customized refrigeration solution for a local seafood processing and export company.The project was designed to support seafood processing, frozen storage, and export distribution. Based onProjects
-
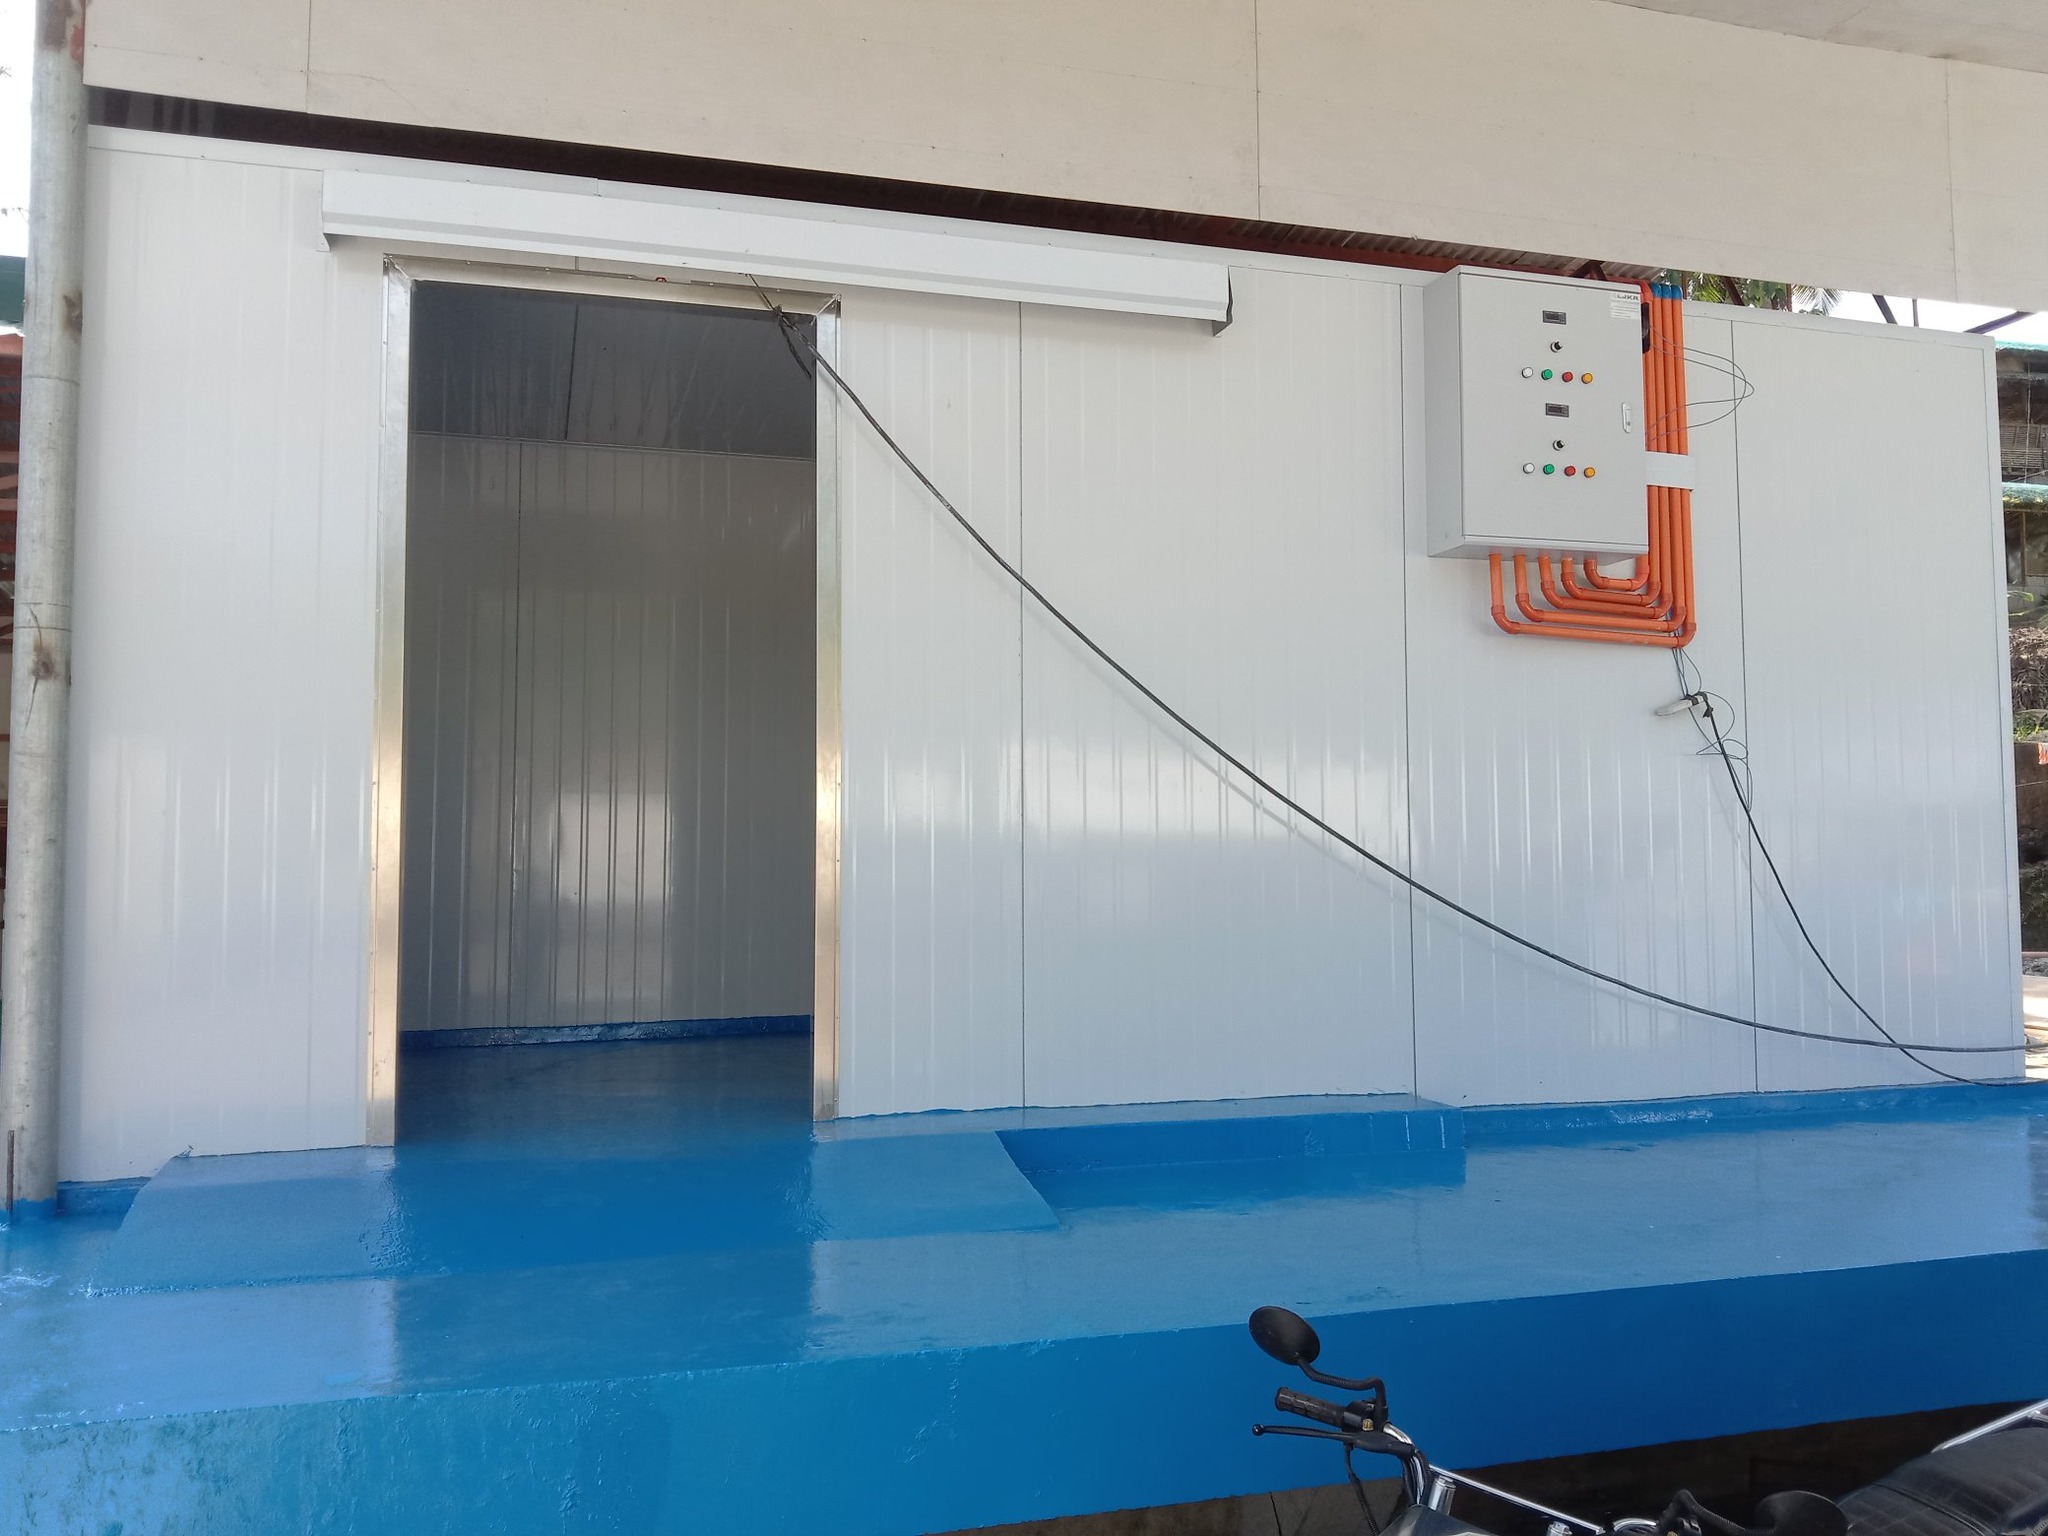 Project OverviewKAIDELI successfully completed a food processing cold storage project in Thailand, providing a complete customized refrigeration solution for a local food manufacturing company.The project was designed to support food processing, chilled storage, and frozen product preservation. BaseProjects
-
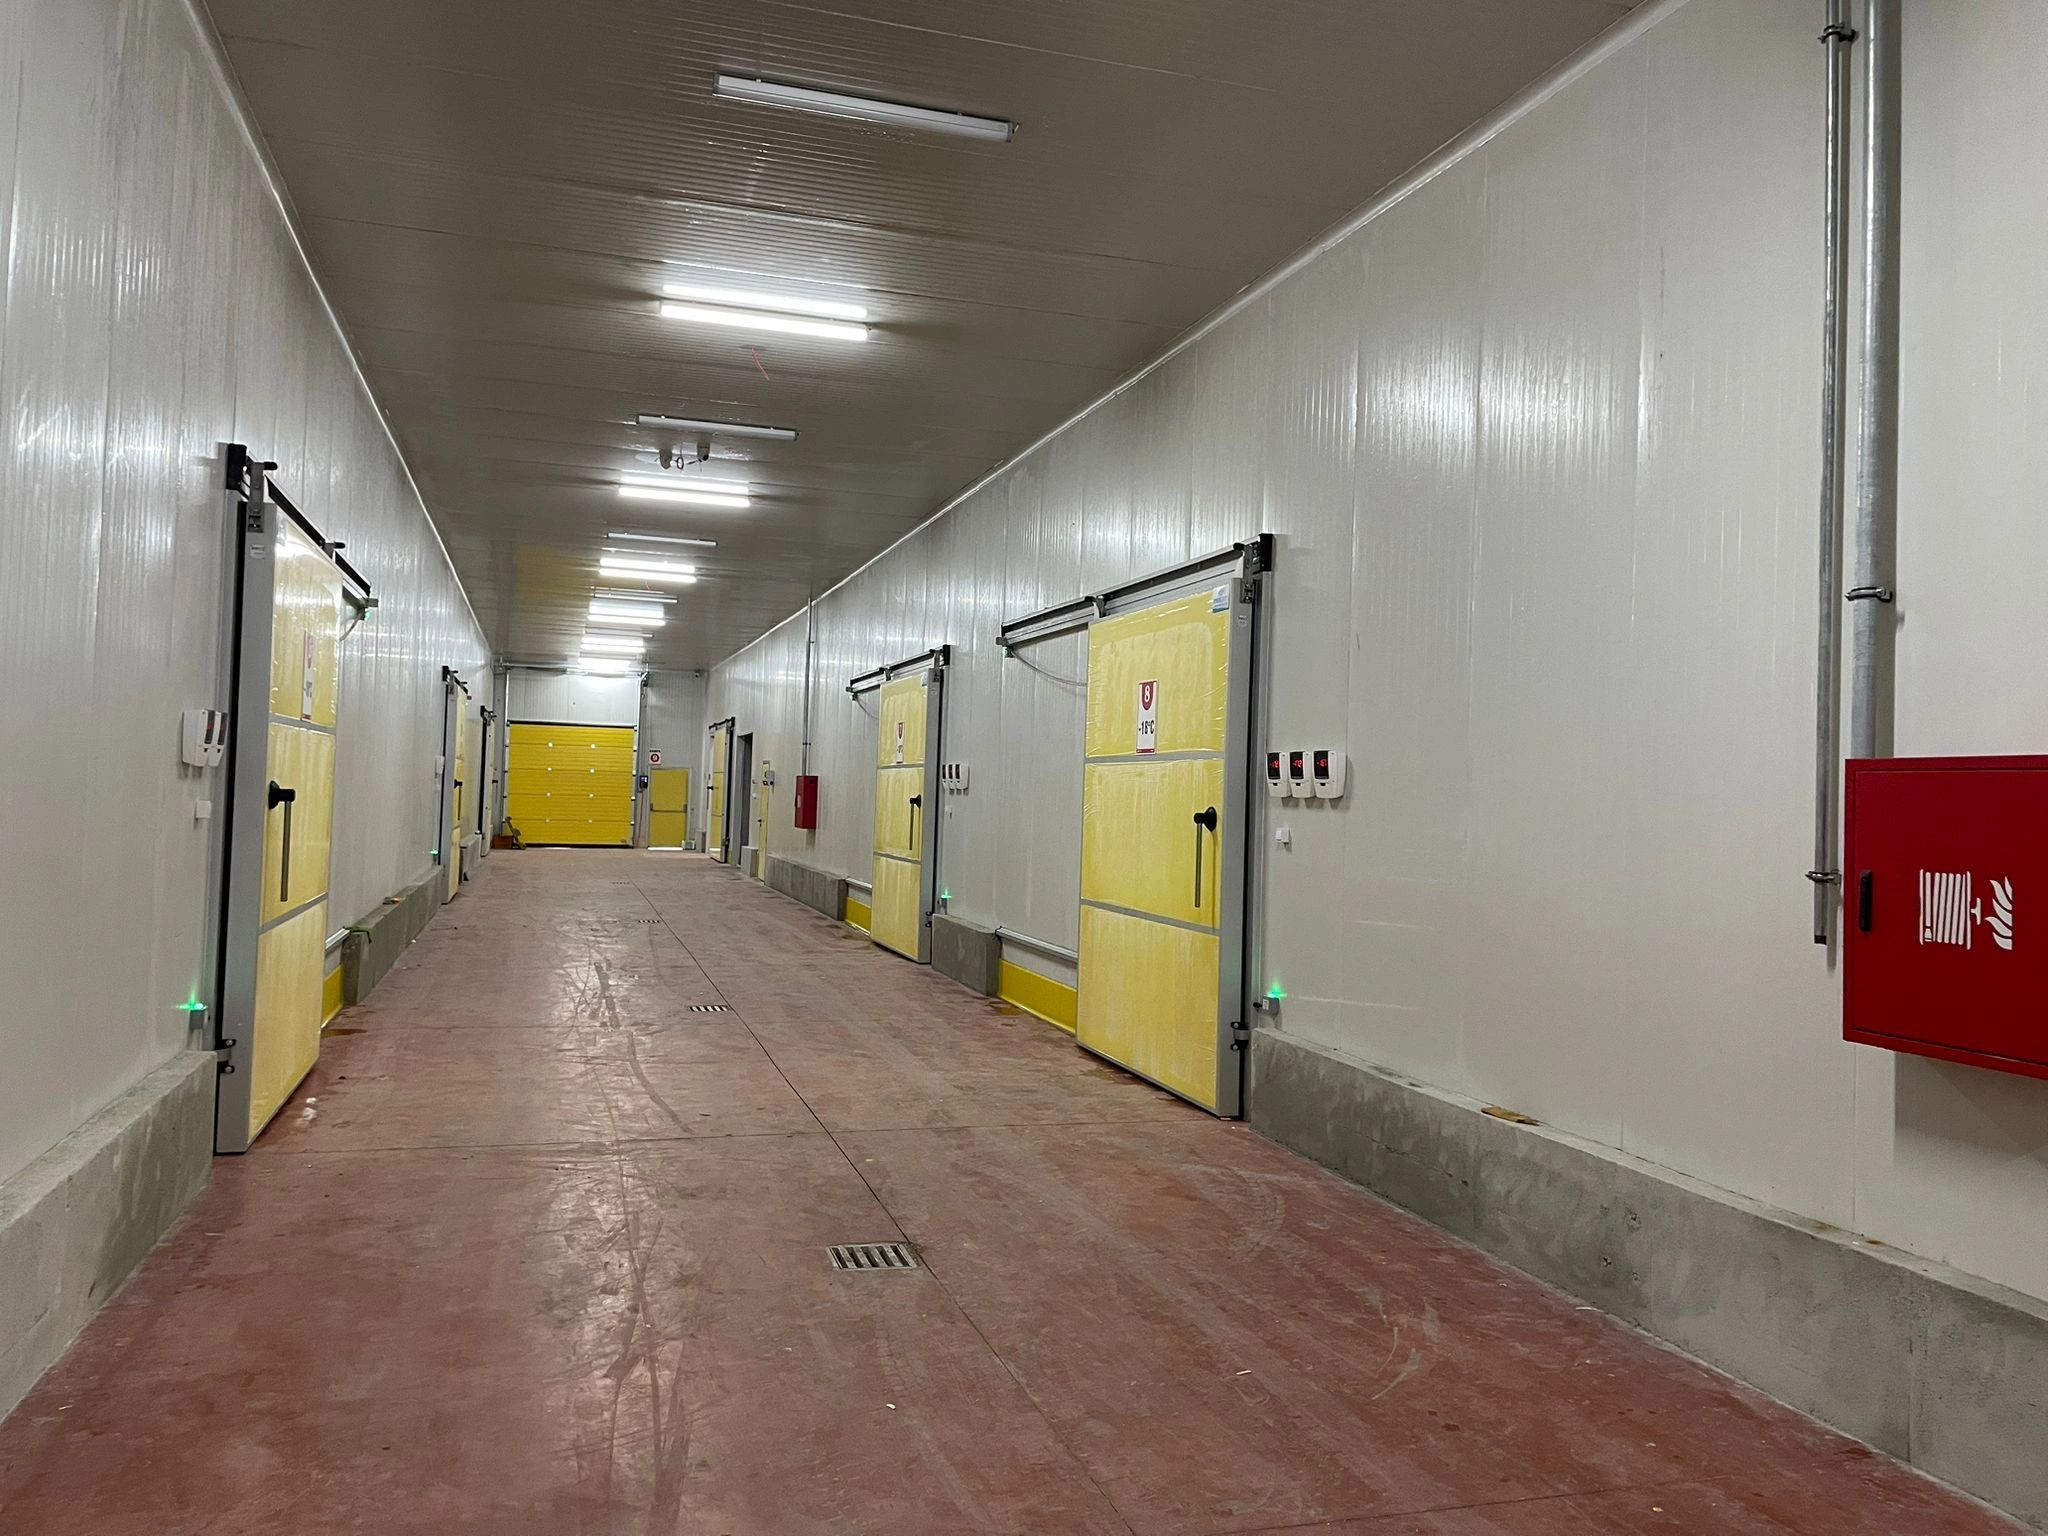 Project OverviewKAIDELI successfully completed a meat freezer warehouse project in Canada, providing a complete customized refrigeration solution for a local meat processing and distribution company.The project was designed to support meat processing, frozen storage, and cold chain distribution. BasProjects
-
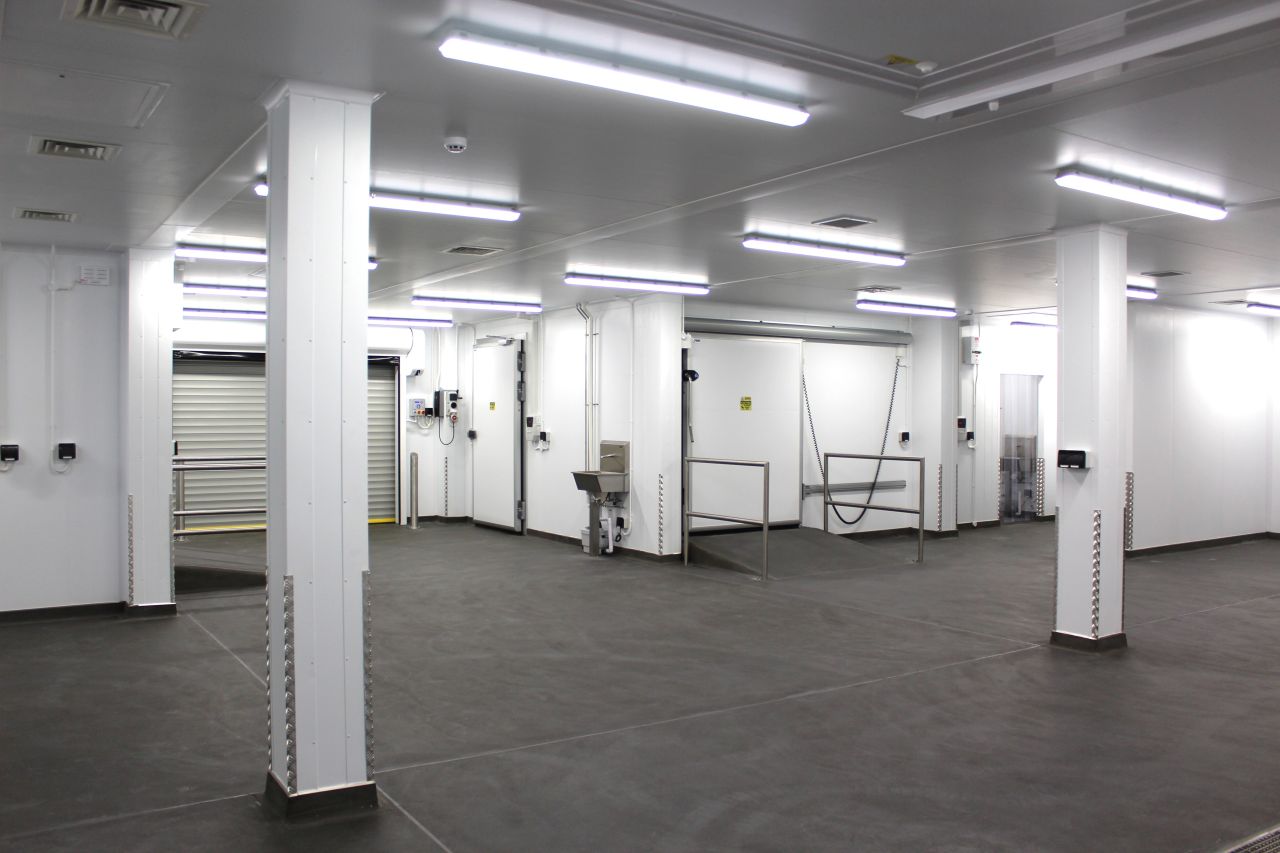 Project OverviewKAIDELI successfully completed a central kitchen cold storage project in the UAE, providing a complete customized refrigeration solution for a large food service company.The project was designed to support food preparation, chilled storage, frozen food preservation, and daily distribProjects


